

Humidity Test Chamber Price: Features, Applications and Buying Guide
A product may perform perfectly under normal environmental conditions but fail when exposed to high humidity or changing moisture levels. This is why humidity testing is an important part of quality control across industries such as pharmaceuticals, electronics, automotive, packaging and research laboratories.
A humidity test chamber helps manufacturers evaluate how products and materials respond to controlled humidity conditions. It allows testing teams to assess moisture resistance, product durability and performance under different environmental conditions.
For businesses planning to invest in this equipment, understanding the humidity test chamber price, features and applications is essential before making a purchase decision.
What Is a Humidity Test Chamber?
A humidity test chamber is a specialised laboratory testing instrument designed to create controlled temperature and relative humidity conditions. It helps manufacturers understand how moisture and environmental changes affect the physical properties, strength and durability of different materials.
The equipment creates a controlled environment inside an enclosed cabinet where samples can be tested for specific durations. This allows quality control teams to identify potential weaknesses before products reach the market.
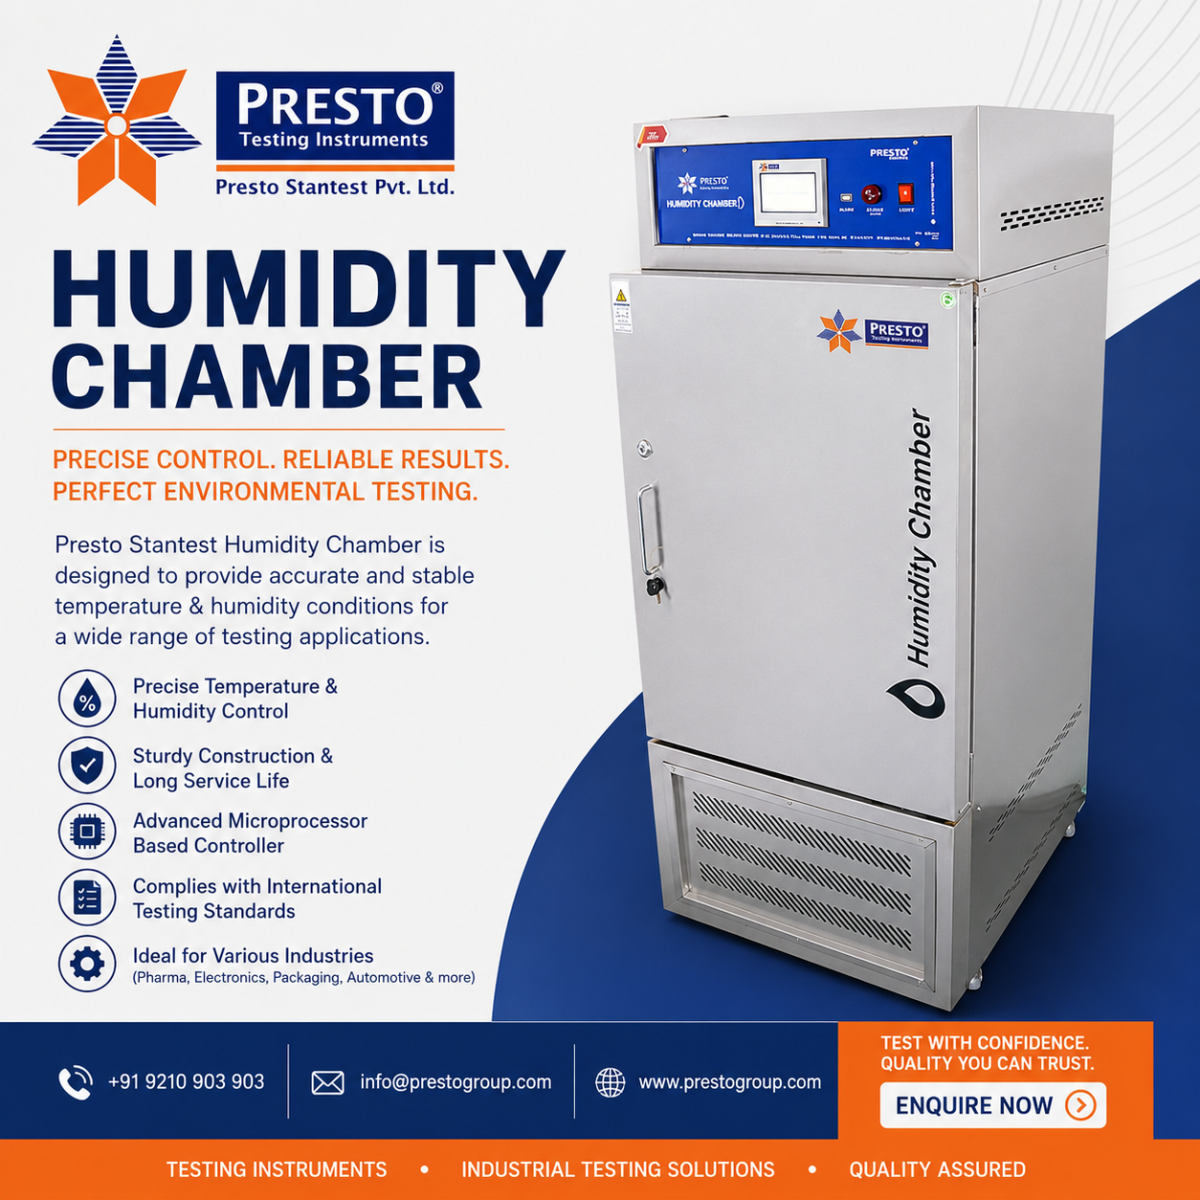
Presto Stantest offers a Humidity Chamber / Conditioning Chamber Prima Series with Touch Screen and Data Logger, designed for reliable environmental conditioning and material testing.
What Factors Affect Humidity Test Chamber Price?
The humidity test chamber price depends on several technical and operational factors. Understanding these factors can help buyers select suitable equipment according to their testing requirements.
1. Chamber Capacity and Size
The internal dimensions of the chamber determine how many samples can be tested simultaneously. Larger chambers generally require more materials, heating capacity and humidity control systems, which can influence the overall cost.
2. Temperature and Humidity Range
Different testing applications require different environmental conditions. A chamber with a wider temperature and humidity range may require advanced control systems and additional components, affecting its price.
3. Control Panel and Automation
Modern humidity chambers feature touchscreen control panels that make it easier to set testing parameters and monitor operating conditions. Automated controls can improve testing convenience and reduce manual intervention.
4. Data Logging Features
Data logging is important for laboratories that need to maintain testing records. Equipment with data recording, graph generation and USB communication capabilities can help users monitor and store test results.
5. Construction and Material Quality
The quality of the internal chamber, insulation, sensors and other components also influences the investment. Stainless steel construction is particularly useful for durability and corrosion resistance.
Important Features of Presto Humidity Test Chamber
The Presto Humidity Chamber Prima Series is designed to provide controlled environmental conditions for material testing and conditioning.
Some of its important specifications and features include:
|
Parameter |
Specification |
|---|---|
|
Model |
PCC-900 Prima |
|
Inside dimensions |
455 × 455 × 710 mm |
|
Display |
HMI-based touchscreen |
|
Temperature range |
15°C to 55°C |
|
Humidity range |
65% to 95% RH |
|
Temperature accuracy |
±2°C |
|
Humidity accuracy |
±5% |
|
Timer |
9999 hours |
|
Sample racks |
2 |
|
Temperature sensor |
PT-100 |
|
Power supply |
220V, single phase |
Additional features include:
-
Inbuilt auto-tuning function.
-
Water-level indicator and low-water alarm.
-
Rapid air circulation for uniform environmental conditions.
-
Inbuilt calibration feature.
-
Automatic stop function.
-
Stainless steel interior and exterior.
-
German-imported fan for efficient air circulation.
The chamber also offers optional configurations, including different capacities and a USB communication port.
These features help laboratories perform controlled humidity testing with convenient monitoring and operation.
Applications of Humidity Test Chambers
A humidity test chamber is used across several industries where product quality and environmental resistance are important.
1. Pharmaceutical Industry
Pharmaceutical manufacturers use humidity chambers to evaluate how moisture and environmental conditions affect the stability and physical properties of different materials and products.
2. Electronics Industry
Electronic components can be affected by moisture exposure. Humidity testing helps manufacturers evaluate the reliability and durability of electronic products under controlled environmental conditions.
3. Automotive Industry
Automotive components may experience changing humidity and temperature conditions during their service life. Testing helps manufacturers assess material performance and identify potential weaknesses.
4. Packaging Industry
Packaging materials need to maintain their strength and performance under different environmental conditions. Humidity testing helps evaluate how moisture affects packaging quality.
5. Research and Development Laboratories
Research laboratories use humidity chambers to study material behaviour, conduct conditioning tests and evaluate product performance under controlled conditions.
How to Choose the Right Humidity Test Chamber?
Before purchasing a humidity test chamber, buyers should consider the following points:
-
Testing requirements: Identify the temperature and humidity conditions required for your application.
-
Sample capacity: Choose chamber dimensions according to the size and number of samples.
-
Accuracy: Check temperature and humidity accuracy to ensure reliable testing.
-
Data recording: Consider data logging and communication features if testing records are important.
-
After-sales support: Select a manufacturer that provides technical assistance, maintenance and service support.
Comparing these factors will help you select equipment that meets your laboratory's requirements without investing in unnecessary features.
Why Choose Presto Stantest Pvt Ltd?
Presto Stantest Pvt Ltd is a manufacturer of testing instruments and laboratory equipment for different industrial applications. Its humidity chamber range is designed to help manufacturers and laboratories evaluate material performance under controlled environmental conditions.
The Prima Series humidity chamber combines touchscreen operation, temperature and humidity monitoring, stainless steel construction and automated features.
With different capacity options available, buyers can discuss their specific testing requirements and select a suitable configuration.
Conclusion
Choosing the right humidity test chamber is an important investment for businesses that want to maintain product quality and improve testing reliability. The humidity test chamber price depends on factors such as chamber capacity, environmental range, accuracy, automation and data logging facilities.
Before making a purchase, compare the technical specifications and ensure that the equipment meets your testing requirements.
If you are looking for a reliable humidity test chamber, explore the Presto Stantest Prima Series and connect with the technical team to discuss your requirements and get the latest pricing.
Explore Product: Humidity Chamber – Touch Screen with Data Logger
Contact Presto Stantest Pvt Ltd
-
Website: https://www.prestogroup.com/
-
Phone: +91 9210 903 903
-
Email: [email protected]






Comments (0)